Meta description: What is SMT in electronics manufacturing? Learn how the surface-mount assembly process works, which SMD packages it uses, how defects are found, and what to check when sourcing components.
On a populated circuit board, tiny resistors, capacitors, and ICs sit on surface pads. A controlled heating process forms the solder joints. Making all those placements and joints consistently depends in part on receiving the exact components the design calls for.
So what is SMT, and what should an engineer or buyer know before a build? The production steps below show where component selection and material handling affect the result.
What Is SMT in Electronics Manufacturing?
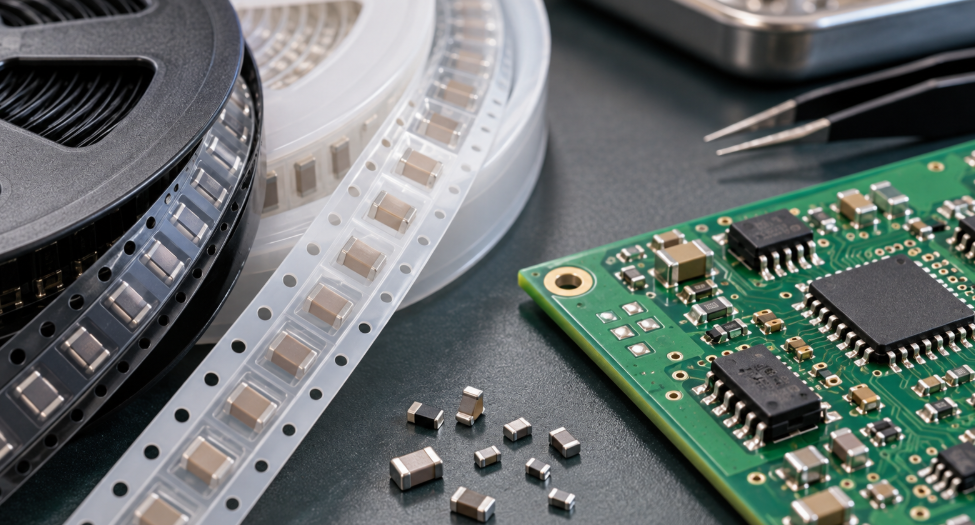
Surface-mount technology (SMT) is a method of assembling electronics in which components are mounted directly on pads on the surface of a printed circuit board (PCB). The component is a surface-mount device (SMD); SMT describes the assembly method. The assembled board is commonly called a PCBA.
SMT is used for many passive parts, semiconductors, and connectors. It supports compact layouts and automated placement, but a board may also include through-hole parts where mechanical or design requirements call for them. A purchasing list should therefore specify the mounting style and full manufacturer part number, not just a generic description such as “10 kΩ resistor” or “8-pin IC.”
How Does the SMT Assembly Process Work?
An SMT line has several linked steps. A defect introduced early can remain hidden until inspection or functional test, so process data should be tied to the same board revision and component lots used in the build.
1. Prepare the PCB and materials
Production starts with the correct PCB revision, stencil, bill of materials (BOM), placement data, and approved component list. Operators load reels or trays into feeders and confirm the material against the work order. For moisture-sensitive packages, they also check the package label and handling status before opening the dry pack.
Buyer check: Confirm the exact part-number suffix, package, quantity, and supply format in the purchase order. A loose-cut strip, full reel, and tray can all contain the same device but require different handling on the line.
2. Print and inspect solder paste
A stencil deposits solder paste onto designated PCB pads. Paste volume and alignment matter: too little paste can contribute to an open joint; excess or misplaced paste can contribute to bridging. Many lines use solder-paste inspection (SPI) at this stage to measure deposits before parts are placed.
3. Place components
Pick-and-place equipment takes parts from feeders, recognizes their orientation, and positions them on the paste deposits. The program must match the correct package footprint and polarity or pin-one orientation. A feeder loaded with a similar-looking but wrong value can turn a placement success into an electrical failure.
4. Reflow, inspect, and test
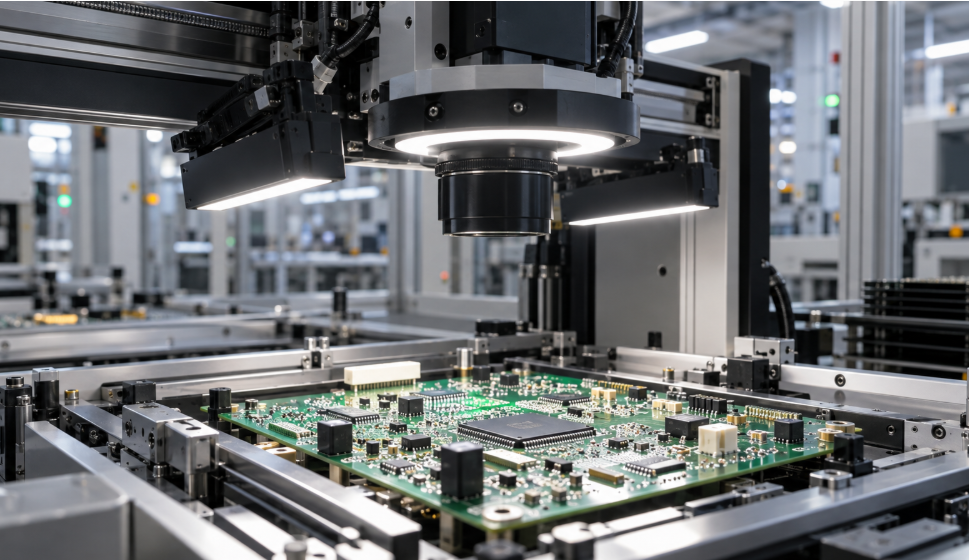
The populated board passes through a controlled reflow profile so the paste forms solder joints, then cools. The profile must suit the paste, PCB, and components; there is no universal oven setting. Automated optical inspection (AOI) can identify visible placement and solder-joint anomalies. For joints hidden under a ball-grid array (BGA) or some leadless packages, an X-ray inspection method may be specified. Electrical, in-circuit, or functional testing can find faults that a camera cannot. Inspection and testing are complementary, and their scope depends on the assembly and its risk.
For the acceptance rules used on a particular build, align the contract manufacturer and customer on the applicable revision and class of IPC J-STD-001 and IPC-A-610. Citing these standards does not by itself prove that a particular board passed inspection.
What Are SMD Components and Common Surface-Mount Packages?
SMDs are components designed for surface mounting. Passive chips, diodes, transistors, ICs, and many connectors come in surface-mount versions. A package name tells you something about physical form; it does not establish electrical interchangeability.
| Package or format | Typical examples | What to confirm before purchase |
|---|---|---|
| Chip passive | Resistors, capacitors, ferrite beads | Size code, value, tolerance, voltage or power rating, termination |
| SOIC, SOT, or similar leaded package | ICs, transistors, diodes | Exact outline, pin count, pinout, lead finish |
| QFN or other leadless package | Controllers, power and RF ICs | Footprint, exposed pad, orientation, assembly guidance |
| BGA | Processors, memories, complex ICs | Ball map, pitch, package revision, moisture handling and inspection plan |
| Surface-mount connector | Board interfaces | Mating geometry, orientation, height, retention, footprint |
The manufacturer datasheet, packaging specification, and approved PCB footprint should agree. Even within one functional family, an extra suffix may change the package, temperature grade, tape orientation, or lead finish. Engineering must approve any substitute; purchasing should not treat a matching package name as a design approval.
SMT vs Through-Hole Technology: What Are the Key Differences?
Through-hole technology (THT) inserts component leads into drilled holes and solders them on the other side of the board. SMT places components onto surface pads. Many products use both methods.
| Decision point | SMT | Through-hole |
|---|---|---|
| Board connection | Surface pads and solder joints | Leads through plated holes |
| Common production approach | Automated paste printing, placement, and reflow | Insertion followed by wave, selective, or manual soldering |
| Layout | Often supports smaller parts and dense layouts | Holes and lead spacing use more board area |
| Mechanical demands | Depends on package and joint design | May suit some connectors or heavy parts requiring lead retention |
| Rework and inspection | Fine-pitch or hidden joints can need specialist equipment | Accessible leads can be easier to hand-solder, depending on board design |
Neither method is automatically the more reliable choice. Pad design, mechanical loading, thermal cycling, solder process, and application requirements decide what works. When reviewing a BOM, distinguish an SMD version from a through-hole version even if the electrical description looks identical.
What Are the Advantages and Limitations of SMT?
SMT can reduce board area, support dense placement, and make high-volume assembly efficient. Shorter connections can also help some high-frequency designs, though circuit performance still depends on the complete layout. Automated placement and process inspection provide useful repeatability when the program and materials are controlled.
The limits are equally practical. Fine-pitch parts demand precise printing and placement. Hidden joints complicate visual inspection. Some large or frequently stressed connectors need additional mechanical support or a different mounting method. Moisture-sensitive packages need handling that matches their manufacturer instructions and applicable IPC/JEDEC J-STD-033 guidance. Do not assume that every SMD has the same moisture sensitivity level (MSL), floor life, or baking rule.
Planning rule: Evaluate the footprint, assembly capability, inspection access, rework plan, and component supply together. A compact package is only useful if the line can build and verify it reliably.
What Defects Can Occur During SMT Assembly, and How Are They Detected?
Common problems include solder bridges, opens or insufficient solder, tombstoned chip parts, shifted components, incorrect polarity, wrong-value placements, and solder voids. A visibly skewed part is an indication to investigate, not enough information by itself to diagnose the root cause.
| Defect or risk | Useful detection point | Follow-up question |
|---|---|---|
| Paste misalignment or uneven deposit | SPI before placement | Was the stencil, paste, or printing setup corrected? |
| Missing, shifted, or reversed part | Placement checks and AOI | Did feeder mapping and polarity data match the BOM? |
| Visible bridge or open joint | AOI and qualified visual review | Does the joint meet the agreed acceptance criteria? |
| Hidden BGA joint anomaly | X-ray where specified; electrical or functional test | Is the inspection method adequate for the joint and failure mode? |
| Wrong electrical value or intermittent function | In-circuit or functional test | Is this a material, assembly, or design issue? |
An inspection image does not guarantee that every electrical fault has been caught. Likewise, a passing functional test may not reveal every latent solder or material issue. Ask your assembler how it records defects, dispositions suspect boards, and connects test results to the PCB revision and component lots. IPC-A-610 provides assembly acceptability criteria, but the applicable customer specification and inspection plan still need to be agreed.
How Do You Choose and Source Components for SMT Production?
Start with the released BOM and the manufacturer’s current datasheet. For each line, verify the manufacturer, full part number, package suffix, electrical rating, footprint, operating temperature, and lifecycle status. Ask engineering to review any proposed alternate for electrical, mechanical, thermal, software, and qualification impacts.
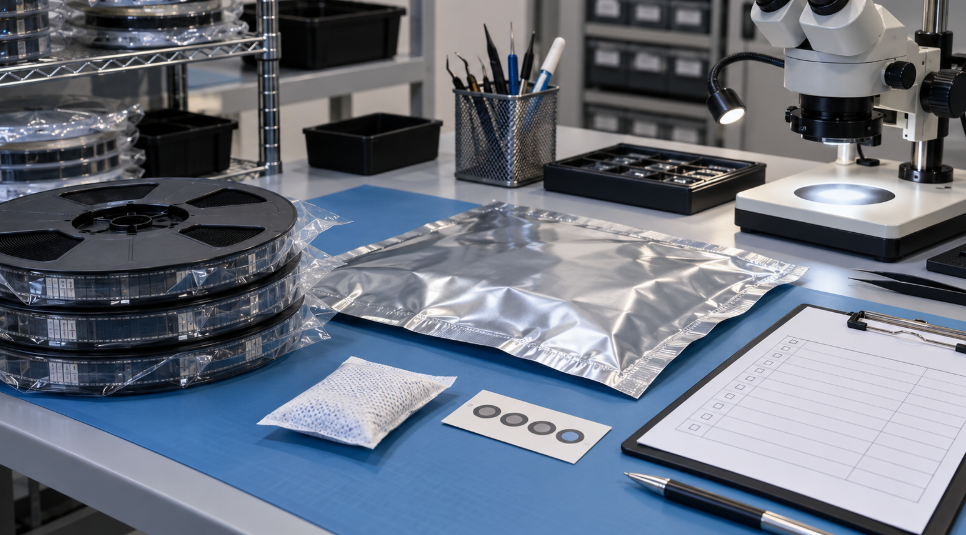
Next, confirm supply details that affect the line: reel or tray format, tape orientation, quantity per package, lot and date-code expectations, and whether material is sealed and labeled as expected. For an MSL-rated device, request the manufacturer MSL information and check the moisture barrier bag, desiccant, humidity indicator, seal condition, and exposure history as applicable. TI explains how its MSL rating and reflow information governs floor-life planning; the exact requirements must be checked for the actual device.
Finally, match the sourcing route to the risk. Verify an authorization claim on the manufacturer’s official channel list. If using an independent supplier, agree in advance what chain-of-custody records, label photos, lot information, inspection, testing, and return terms can actually be provided. Evidence varies by source; a photo or certificate alone is not proof of authenticity. For a repeat build, record approved alternates and supply formats in the BOM procurement plan so an urgent shortage does not force a guess at the feeder.
Conclusion
SMT production depends on accurate board data, the right components, process controls, and an inspection plan. A buyer can prevent a common line stoppage by checking the package and handling details before approving an order. DuoLink Electronics is an independent electronic-components supplier offering BOM quotation and sourcing support. For an SMT build, send us your BOM or part-number inquiry with full part numbers, quantities, application, packaging needs, and required documentation so the available options can be checked against your build requirements.
Frequently Asked Questions
Is SMT the same as SMD?
No. SMT is the assembly method; an SMD is a component intended for surface mounting.
Can the same PCB contain SMT and through-hole parts?
Yes. Many assemblies combine them. The process sequence and soldering method should be planned with the assembler.
Does every SMT component need dry-pack handling?
No. Check the specific manufacturer’s package and MSL guidance. Do not assign a floor life from a generic package name.
Does AOI inspect solder joints under a BGA?
Conventional optical inspection cannot see concealed joints directly. An approved X-ray method and electrical or functional tests may be used according to the risk and inspection plan.
Can a buyer replace a component with one in the same package?
Not without engineering review. Package fit does not confirm pinout, ratings, firmware compatibility, qualification, or lifecycle suitability.


 English
 German
 Spanish
 French
 Chinese
 Italian