A supplier may list millions of electronic components on its website. That figure does not tell you how many parts are ready to ship.
Some parts may be sitting in the supplier’s warehouse. Others may belong to partner distributors, manufacturers, traders, or inventory holders in another country. In some cases, the supplier does not purchase the material until it receives your order.
For a buyer, those differences matter. Your production plan depends on a specific manufacturer part number, quantity, package, date code, condition, and delivery date. A number in an online catalog cannot confirm any of these points.
When I evaluate component inventory, I start with a few direct questions: Where are the parts? Who owns them? Has someone checked the physical quantity? What documents follow the stock? The answers usually tell you more than the size of the supplier’s online database.
Why inventory evaluation matters when choosing a component supplier
Inventory size does not always equal availability
Many electronic component websites use searchable databases rather than live warehouse records. One search result may combine stock from several sources.
| Inventory type | What it means | What you should confirm |
|---|---|---|
| Supplier-owned stock | The supplier physically holds the parts | Quantity, warehouse location, lot details, and packaging condition |
| Partner stock | A cooperating supplier or distributor holds the parts | Who controls the stock and whether it can be reserved |
| Global network stock | The result comes from several regional channels | Source, lead time, traceability, and when availability was last checked |
| Market-sourced stock | The supplier will purchase the parts after receiving your order | Final source, inspection process, and the risk of stock changes |
A broad inventory database can show that a supplier has access to many sourcing channels. It does not prove that every listed part is available.
Instead of asking how many part numbers the company carries, ask which parts have been physically checked and can be allocated to your order.
This point becomes more important when you are purchasing obsolete ICs, discontinued semiconductors, automotive-grade devices, or shortage parts. These components may pass through several companies before reaching the final buyer.
How poor inventory information affects production
Unclear stock information can cause problems before anything is shipped.
The quoted stock may already have been sold. The quantity may be divided between several warehouses. A reel described as factory sealed may have been opened and resealed. The supplier may offer a part with a different suffix because the base model looks the same.
Each difference carries its own production risk. A different package may not fit the PCB footprint. The temperature grade may fall outside the equipment’s operating range. Mixed date codes may conflict with your customer’s approval rules. Loose parts may be unsuitable for automatic placement.
For buyers sourcing parts for industrial automation systems, one incorrect component can delay assembly, maintenance work, testing, or equipment delivery.
Inventory risks in the independent distribution market
Independent distributors can locate shortage, obsolete, and difficult to source components that are no longer available through normal channels. The level of risk depends on where the stock came from and how the supplier controls it.
A supplier should tell you whether the material comes from its warehouse, an authorized distributor, an OEM excess inventory source, a contract manufacturer, or another independent channel. “Available stock” is too vague to support a purchasing decision.
The source should also affect the inspection plan. Factory-sealed stock with continuous traceability does not carry the same risk as an opened reel obtained through the secondary market. Either may be usable, but they should not go through the same approval process.
Determine whether the inventory is actually available
On-hand stock, partner stock, and market-sourced stock
Before discussing delivery, ask the supplier to classify the inventory.
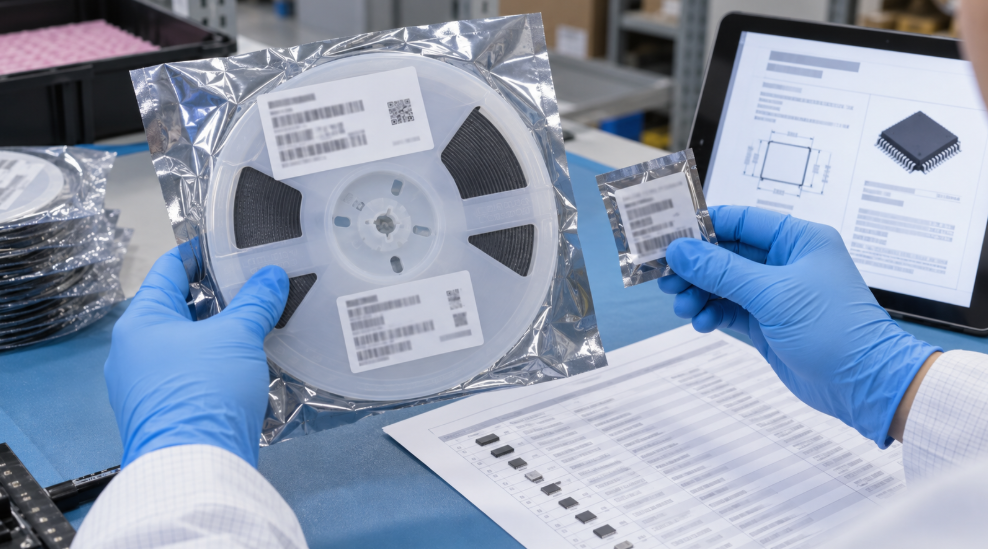
You need to know whether the parts are physically on hand, whether the quantity has been checked, and whether another customer has already reserved the stock. The reply should also identify the warehouse country and explain whether the supplier controls the goods or still needs to purchase them.
Partner stock can change quickly. Ask when the supplier last checked the quantity. A database record from several weeks ago should not be treated as current stock.
If the supplier plans to purchase the material after receiving your order, ask how it selects the source and what inspection will take place. Market sourcing can work, especially for shortage parts, but you need to know if the source changes after you approve the offer.
Ask for the current quantity and warehouse location
Warehouse location affects delivery time, inspection access, export documents, and the supplier’s control over the goods.
Check whether the quoted quantity refers to usable units or only the amount shown in a database. A listing for 10,000 pieces may consist of several partial reels held by different sellers. Some units may already be allocated, damaged, or packed in a format that does not meet your assembly needs.
For production orders, ask the supplier to confirm the shippable quantity after checking the physical stock.
If you require full reels, original trays, continuous tape, or a certain leader length, include those conditions in the RFQ and purchase order. Otherwise, the supplier may provide the correct component in packaging that your production line cannot use.
Request time-stamped inventory evidence
Current photographs and videos can help you determine whether the supplier controls the stock or is repeating information from another database.
| Evidence | What it helps confirm | What it cannot confirm by itself |
|---|---|---|
| Time-stamped stock photo | Physical possession, packaging, and approximate quantity | Authenticity or electrical performance |
| Label close-up | Part number, date code, lot code, quantity, and packaging details | Whether the label covers the entire offered quantity |
| Warehouse video | Physical location, seal condition, and visible stock | Full traceability or internal component condition |
| ERP screenshot | Recorded quantity and warehouse reference | Whether the system record matches the physical goods |
| Packing list or source document | Previous movement through the supply chain | Authenticity when the document cannot be linked to the parts |
Ask the supplier to place a dated note or your RFQ number next to the material. This makes it harder to reuse an old stock photo from another inquiry.
Do not approve an order from one polished photograph. Review the photos together with the labels, source documents, inspection results, and test reports required for the application.
Verify part numbers and inventory data accuracy
Confirm the complete manufacturer part number
Electronic components must be checked by the complete manufacturer part number, not only the product family or base series.
A suffix may define the package, temperature range, voltage option, speed grade, lead finish, qualification level, programming state, or packing method. One missing letter can describe a different orderable part.
Compare the quotation with the BOM character by character. Review the manufacturer, full part number, package, pin count, electrical rating, temperature grade, tolerance, lead-free status, and packaging format.
This review is especially important for integrated circuits and processors. Two codes that look almost identical may refer to different packages or operating grades.
Distributor product titles are not enough. Check the orderable code against the manufacturer’s datasheet, package drawing, and product change information. For discontinued stock, confirm which datasheet revision applies to its manufacturing date.
Check package, grade, and technical specifications
One component family may include commercial, industrial, automotive, or military grades. These versions can share a base number while using different qualification requirements, operating temperatures, screening processes, and supporting documents.
The packaging format also affects production. Reels, trays, tubes, and cut tape require different handling and assembly processes. Components removed from the original packaging may need counting, lead inspection, solderability review, or repacking before use.
Write the required condition in your RFQ. “New and original” leaves too much room for interpretation.
State whether you need factory-sealed packaging, a single lot, a certain date-code range, full traceability, an authorized source, or a test report linked to the offered stock.
Separate approved alternatives from exact matches
If the original part is unavailable, the supplier may offer another component with similar specifications. Record it as a proposed alternative rather than an exact match.
Engineering should check the electrical function, pinout, package dimensions, firmware compatibility, qualification status, environmental compliance, and operating conditions.
The inventory file should place exact matches and alternatives in separate columns. This prevents purchasing staff from ordering an unapproved substitute because both items appeared on the same quotation.
Review date codes, lot codes, and inventory consistency
Check manufacturing date and lot information
A date code normally identifies the manufacturing period. A lot code connects the component to a production batch or manufacturing record. Formats differ between manufacturers and product families, so one decoding method will not work for every brand.
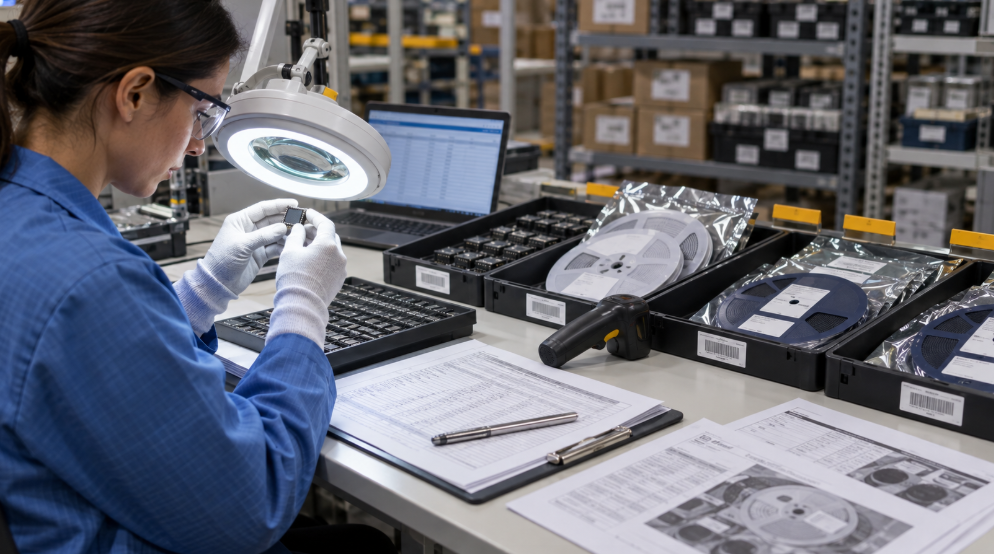
Request clear images of the packaging labels. Where inspection allows, compare the information on the carton, reel, moisture barrier bag, tray, and component body. The records should be consistent.
A recent date code does not prove that a part is better. An older genuine component stored in suitable conditions may be more reliable than a recently remarked or poorly handled part.
Date code is one part of the review. Storage, packaging, component type, and intended application matter as well.
Identify mixed-lot or mixed-date-code inventory
The quantity on one quotation line may come from several manufacturing lots.
Mixed inventory may be acceptable for many commercial products. It can still create more work for incoming inspection, process validation, traceability, and customer approval.
Ask the supplier how many date codes and lot codes are included. Confirm the quantity in each lot and whether all lots came from the same source. The warehouse should keep them separated during inspection, packing, and shipment.
If your project requires one lot, write that requirement before the supplier reserves the material. Do not assume that one quotation line means one manufacturing lot.
Buyers should apply stricter controls to components used in automotive, medical, aerospace, safety-related, or long-life industrial products. The final requirements depend on the application and the customer’s approval process.
Decide whether older stock is suitable
Age alone does not decide whether inventory is usable. Review the component type, storage history, packaging condition, termination finish, moisture sensitivity, and application risk.
Semiconductors in intact original packaging may remain usable for a long time. Other component types need different checks. Oxidized leads can affect solderability. Electrolytic capacitors may need more assessment after extended storage. Relays and connectors can develop contact or material problems. Moisture-sensitive devices may absorb moisture once the protective bag is opened.
Ask when the package was opened, whether the parts were dry-packed again, and whether the supplier has storage records.
Long-stored or higher-risk stock may need visual inspection, solderability testing, X-ray inspection, electrical testing, decapsulation, or another method selected for the component.
Rejecting every older date code may remove legitimate supply options. Accepting old stock without checking its history creates an avoidable production risk.
Evaluate traceability and source documentation
Identify the original inventory source
Traceability shows how far you can follow a component through the supply chain.
Strong records may connect the stock to the original manufacturer or an authorized distributor. Limited records may identify only the supplier’s immediate source.
Ask the supplier to describe the source category. If it cannot disclose the company name for commercial reasons, it should still state the channel type, country, purchase date, and available documentation. “Confidential source” should not mean that no source information exists.
The required level of traceability depends on the end use. A maintenance component for non-safety equipment may have different requirements from a part used in a medical device, vehicle, or aerospace system.
Review certificates and supporting documents
Supporting records may include manufacturer labels, authorized distributor labels, packing lists, purchase records, Certificates of Conformance, inspection reports, test reports, and lot documents.
A Certificate of Conformance supports the transaction, but it does not prove authenticity on its own. Check who issued it, which purchase order it covers, and whether its part number, quantity, date code, and lot information match the goods.
Photos taken before repacking can also help. If the supplier baked, relabeled, resealed, or converted the parts to tape and reel, request records of that work.
The ECIA explanation of SAE AS6496 discusses traceability records, date and lot-code matching, packaging inspection, and the handling of returned parts within authorized distribution.
AS6496 applies to authorized or franchised distribution. An independent distributor should not claim this certification unless the claim is valid. For independent-channel orders, ask which standards and internal procedures cover sourcing, inspection, suspect parts, and record retention.
Look for gaps in the chain of custody
A gap exists when part of the material’s history cannot be supported.
You may find a missing original label, an unexplained quantity change, inconsistent document dates, or packaging that does not match the stated source. One gap does not prove that a component is counterfeit, but it raises the sourcing risk.
Ask the supplier to explain the inconsistency in writing. Based on the answer, you may need deeper inspection, sample testing, third-party laboratory analysis, customer approval, or another stock source.
The supplier should disclose these gaps before shipment. Buyers should not have to discover them during incoming inspection.
Inspect storage, handling, and packaging conditions
Check ESD and moisture protection
A genuine component can still fail after poor handling.
Electrostatic discharge may damage a sensitive device without leaving a visible mark. Moisture absorbed by a package can lead to cracking, delamination, or internal damage during reflow.
Ask whether staff handle unpackaged ESD-sensitive components inside an ESD-protected area. Review the use of grounded workstations, personnel grounding, protective containers, staff training, and monitoring records.
The EOS/ESD Association explains that ANSI/ESD S20.20 principles cover work areas, personnel grounding, packaging, and the handling of ESD-sensitive items.
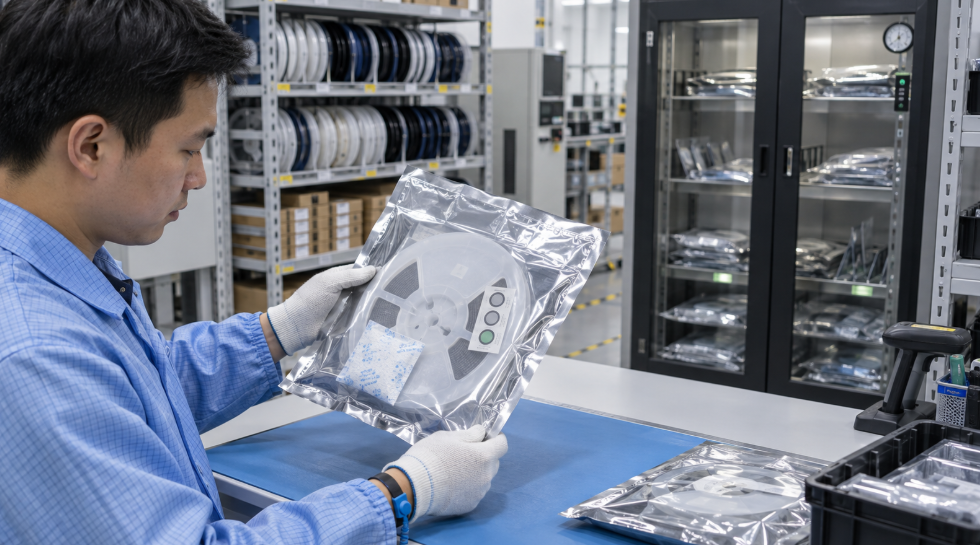
For moisture-sensitive devices, inspect the moisture barrier bag, desiccant, humidity indicator card, seal date, sensitivity label, and floor-life information.
The IPC/JEDEC J-STD-033 standard covers the handling, packing, shipping, and use of moisture-sensitive, reflow-sensitive, and process-sensitive devices.
A vacuum-sealed bag is not automatically compliant dry packing. Bag material, seal condition, labeling, desiccant, and humidity indication all need to be checked.
Examine original packaging and seal integrity
Original packaging can support identification and traceability, but it still requires inspection.
Check for broken or doubled seals, labels placed over older labels, unusual fonts, inconsistent logos, handwritten quantity changes, damaged reels, and missing humidity indicator cards.
Look at pocket orientation and cover-tape condition as well. Parts transferred to another reel or tray should not be described as untouched original packaging.
Repacking is sometimes necessary. A supplier may split a quantity, replace damaged packaging, or prepare cut tape for a smaller order. The work should be disclosed and recorded, with suitable ESD and moisture controls used throughout the process.
Ask how sensitive components are stored
A warehouse photograph cannot show how the supplier controls temperature, humidity, opened packages, and ESD-sensitive inventory.
Ask about temperature and humidity monitoring, dry cabinets, ESD-protected work areas, floor-life tracking, stock rotation, quarantine areas, and the separation of inspected and uninspected material.
Buyers often spend more time reviewing markings than storage history. I would check both. A genuine IC left exposed to humidity can still cause problems during placement or reflow.
Identity and physical condition are two separate parts of inventory approval.
Test the supplier’s ability to fulfill the inventory
Start with samples or a controlled trial order
For a new supplier or an unfamiliar source, begin with a manageable quantity.
A trial order lets you compare the delivered material with the quotation, photographs, labels, date codes, packaging description, and promised documents.
Make sure the sample comes from the same lot offered for the production order. A sample selected from unrelated stock tells you little about the remaining quantity.
Before approving the balance, record the accepted part number, lot, date code, packaging, inspection result, and photographs. Ask the supplier to reserve the remaining stock and obtain written approval before changing the lot.
Confirm inspection and testing options
Choose the inspection method according to the component and the sourcing risk.
Some orders only need a label review, packaging inspection, and external visual examination. Parts from higher-risk channels may need dimensional checks, marking inspection, X-ray analysis, solderability testing, electrical testing, XRF analysis, decapsulation, or die inspection.
Ask who performs each test, which procedure is used, and how many parts will be sampled. The final report should identify the lot and quantity that were inspected.
A generic laboratory report has limited use if the supplier cannot connect it to the components in your order.
You can review the supplier’s component sourcing and verification capabilities before submitting a BOM or requesting a difficult-to-source part.
Use an inventory evaluation checklist before purchase
| Evaluation area | Questions to answer |
|---|---|
| Availability | Has the supplier physically confirmed the quantity? |
| Ownership | Is the stock supplier-owned, partner-held, or market-sourced? |
| Identification | Does the full manufacturer part number match the BOM? |
| Lot consistency | How many date codes and lot codes are included? |
| Condition | Is the packaging sealed, opened, repacked, or damaged? |
| Traceability | Which source records and certificates are available? |
| Storage | Were ESD-sensitive and moisture-sensitive parts handled correctly? |
| Inspection | What checks will take place before shipment? |
| Testing | Does the test plan match the component and source risk? |
| Fulfillment | Can the supplier ship the approved lot without substitution? |
A supplier should be able to answer these questions without hiding behind a stock number or a general promise.
Fast replies help when parts are scarce, but accuracy matters more. Resolve unclear source information, lot details, packaging condition, and inspection requirements before issuing the purchase order.
Work with Duolink Electronics on your component requirements
Evaluating inventory requires more than finding a part number in a catalog. You need to confirm physical availability, complete ordering codes, lot information, source records, packaging, storage, and the inspection process.
Duolink Electronics is an independent electronic component supplier. We source integrated circuits, semiconductors, passive components, connectors, and other electronic parts.
Our team supports overseas buyers with BOM sourcing, part-number checks, inventory inquiries, alternative-part review, and components that are difficult to obtain.
If you are looking for electronic components, submit the required part numbers, quantities, packaging preferences, and documentation needs through our website. We will review the request and confirm the available sourcing options.
Frequently asked questions
How can I tell whether a supplier physically holds the components?
Request the warehouse location, current quantity, time-stamped photographs, label close-ups, and a short video showing your RFQ number beside the stock. Ask whether the supplier owns the material or is checking a partner’s inventory.
Is a recent date code always better?
No. A date code does not determine quality by itself. Check storage history, packaging condition, moisture exposure, solderability, lot consistency, component type, and the final application.
Can I accept mixed date codes in one production order?
You can accept them if engineering, quality staff, and the end customer allow mixed lots. Ask for the quantity in each date and lot code, keep the lots separated, and agree on testing before shipment.
Does a Certificate of Conformance prove that parts are genuine?
No. Compare the certificate with the issuer, source, part number, quantity, lot details, purchase order, and physical material. It is one supporting record rather than standalone proof.
What tests should I request for independent-channel components?
The test plan depends on the part, source, application, value, packaging condition, and available traceability. Options include label checks, visual inspection, X-ray analysis, electrical testing, solderability testing, XRF analysis, and decapsulation.
Should I reject inventory if the supplier cannot provide full traceability?
Limited traceability raises the risk but does not always require automatic rejection. You may need more inspection, laboratory testing, customer approval, or a smaller trial order. Regulated and safety-related applications may require complete documentation.
 English
 German
 Spanish
 French
 Chinese
 Italian